TIG welding
across Dallas–Fort Worth
TIG welding
across Dallas–Fort Worth
Home / About
DFW TIG Welding is built around one process. TIG is slower than the alternatives, and that's the point: the welder controls the heat, the filler and the finish separately, which is what aluminum, stainless, thin steel and chromoly need. They're the metals that punish rushing.
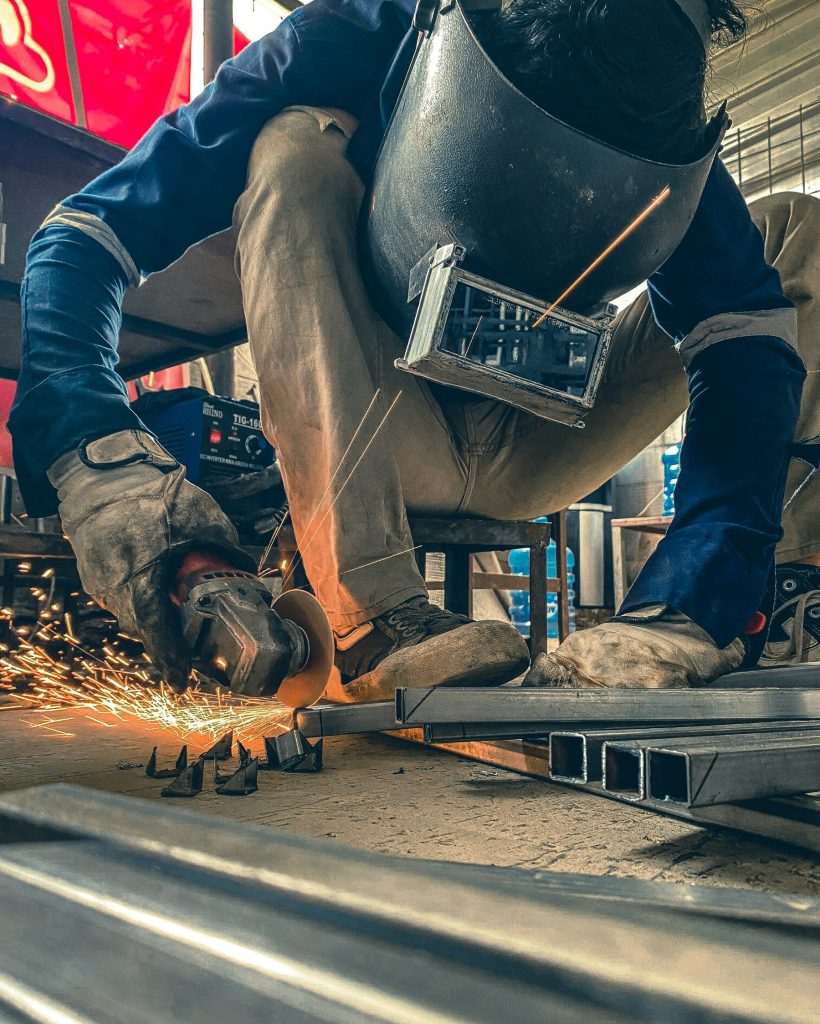
Small parts get the bench: fixtures, good light and time.
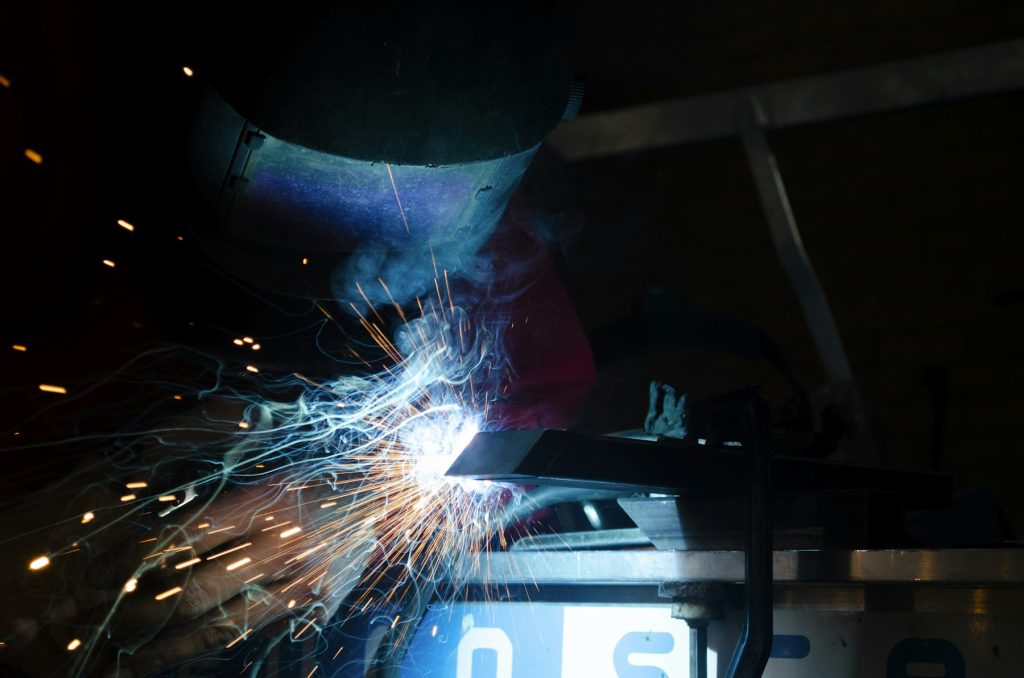
Rod in one hand, torch in the other, heat on the foot pedal.
1.
We'd rather ask two questions than guess. A clear photo and a measurement get you an actual number, not a wide range that only protects the welder.
2.
Grinding out a crack, scrubbing off oxide, fitting the joint tight. Nobody sees this part, and it's the reason a weld holds.
3.
Too much heat warps sheet, burns through tube and leaves stainless open to rust. Short, controlled passes take longer and come out straighter.
4.
Some parts shouldn't be welded: certain heat-treated pieces, safety-rated components, things worn past saving. When that's the case we say so, and point you somewhere useful.
The bench gives us full control: fixtures, back-purge gas, good light and no wind. If the part can travel, this is usually the cheaper option and the cleaner result.
Gates, railings, kitchen equipment, trailers and anything bolted down. We bring a portable TIG setup and gas, and screen the work from wind.
Work with us
Send a few photos and tell us what the part does. You'll get questions or a quote back.